More design freedom for custom aluminium profiles
From 150 to 200 mm
An extra 50 mm in profile height may not sound like much. But for an engineer, an increase of over 30% can open up new design possibilities.
With a targeted upgrade to our existing stretching equipment, we are increasing the profile height capacity at BOAL Extrusion in De Lier from 150 to 200 mm. This allows us to make better use of the technical capabilities of our existing 8-inch extrusion press, without replacing the entire installation.
But the additional profile height is not the only benefit. The upgrade gives us even greater control over the stretching process, helps us further reduce material loss and enables us to produce more profiles locally in De Lier.
For customers, this means greater technical freedom in profile design, a reliable production process and more opportunities to organise production closer to the market.

More freedom to design
For us, a good aluminium profile does not start at the extrusion press. It starts with understanding what the profile needs to do.
What loads will it need to withstand? How will it be assembled? Where is material really needed? And where could the design perhaps be smarter or lighter?
That is why we prefer to get involved while a customer's profile is still an idea or an initial design. By considering geometry, alloy selection, wall thicknesses, tolerances and production capabilities at an early stage, we can work together to find the right balance: lightweight where possible, strong where necessary and manufacturable through a reliable production process.
That last point matters. After all, a cleverly designed profile must also be possible to manufacture.
The stretcher upgrade gives us greater technical flexibility. Previously, we could process profiles up to a maximum height of 150 mm after extrusion. We can now process profiles up to 180 mm, allowing us to make better use of the available capacity of our 8-inch press.
For engineers, this means that production limitations are less likely to restrict the search for the most suitable profile geometry.
This additional 20% also addresses a profile height range for which there is clear customer demand. It expands our capabilities for custom aluminium profiles in sectors including horticulture, solar, transport, building and construction, and electrical engineering.
What actually happens during stretching?
After a profile has been extruded and cooled on the cooling table, it is stretched before moving on to further processing.
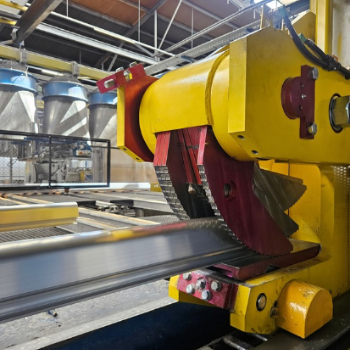
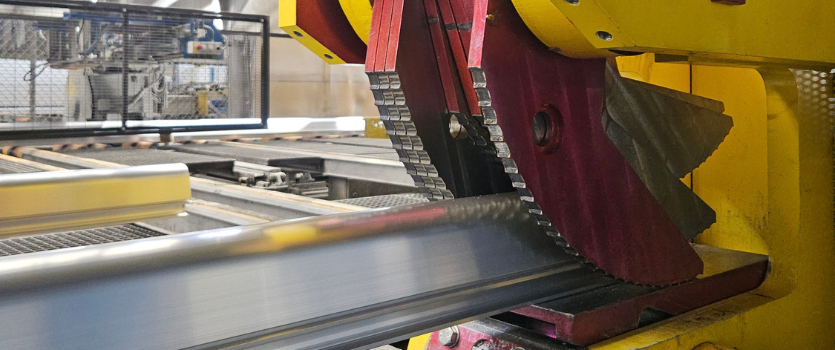
The installation consists of two sections: a fixed tail stretcher at the end of the cooling table and a movable head stretcher at the beginning. The profile is clamped at both ends and then subjected to controlled tension to straighten it.
The upgrade does more than enable us to process taller profiles. It also gives us greater control over how the profile is held and stretched. The forces can be distributed more evenly across the profile, further reducing deformation and providing a more stable starting point for the machining and assembly operations that follow.
"You can put a great deal of effort into designing an efficient profile, but you obviously don't want to lose unnecessary material during production."
Rob Ansems - Maintenance ManagerSmart material use does not stop at the drawing board
Many improvements can already be achieved during the design stage. But when you have worked together to use aluminium as efficiently as possible in a profile, you naturally want to avoid unnecessary material loss further down the production process.
This is where the upgrade delivers a second important benefit.
"You can put a great deal of effort into designing an efficient profile, but you obviously don't want to lose unnecessary material during production," explains Rob Ansems, Maintenance Manager at BOAL Extrusion.
"With the upgraded stretcher jaws, we have greater control over the stretching process. This allows us to further reduce deformation and stretching losses. When a profile leaves this stage of the process in a more stable condition, it also provides a better starting point for the operations that follow."
In that sense, smart material use runs throughout the entire process: from the very first design decisions to the moment a profile leaves the production line. Using aluminium where it is needed, while minimising unnecessary material consumption and loss wherever possible.
More local production
One practical advantage of the increased profile height capacity can be seen in the horticultural sector. We regularly produce aluminium profiles with greater heights for several customers in this market.
Previously, some of these profiles could not be processed entirely in De Lier because of the limitations of our existing stretching equipment. As a result, they were produced by our colleagues at BOAL Extrusion in Shepshed, United Kingdom.
Following the upgrade, more of this production can now take place entirely in De Lier. This shortens the production chain and reduces transport movements between the two sites. At the same time, it frees up capacity in Shepshed for custom production serving the British market.
Robert Draisma, Managing Director of BOAL Extrusion Netherlands, explains:
"Local4Local sounds simple, but it requires production sites to have the technical capabilities to fulfil that role. If a product for this market can be manufactured in De Lier, that is where we want to make it. And if doing so creates more capacity in Shepshed for local British customers, we are making better use of our capacity as a group while avoiding unnecessary transport movements."
Greater control with fewer manual operations
The stretching process has also been further automated. This reduces the need for manual operations and allows the process to be carried out more consistently.
For customers, this ultimately translates into something very practical: a production process designed to be as stable as possible, supporting consistent, repeatable quality and production continuity.
Safety and ease of maintenance were considered from the outset. For the engineering and implementation of the upgrade, BOAL worked with the Italian company SMF, a specialist in solutions for aluminium extrusion lines. The aim was to retain as much of the existing production environment as possible, while making targeted improvements where they would add technical value.
And the project moved quickly…
In week 9, the team began its initial assessment. By week 10, the CAPEX business case was ready. The final design was approved in week 16, the upgraded components were shipped from Italy in week 32, and installation and integration took place in De Lier in week 33.
Less than six months after the first concrete plans were developed, the upgraded stretching equipment was operational.
For Robert Draisma, the upgrade is a clear example of how BOAL aims to continue developing its production capabilities, step by step:
"The manufacturing industry faces the challenge of producing efficiently, flexibly and responsibly, all at the same time. That is not something you achieve in one big step. It comes from continuing to invest in technology, people and processes that deliver measurable improvements. More possibilities for our customers, less waste and a production organisation that is better prepared for what the market will demand tomorrow. That is what we want to keep building on."
Read more
A consistent approach to leadership
Good leadership starts with understanding what people need. Particularly in a manufacturing environment, where employees with different backgrounds, e...
Read more
Why aluminium matters in the next phase of European solar
The European solar industry is maturing. For years, the sector was assessed mainly on its contribution to clean energy. Today, however, there is also...
Read more
Geopolitical tensions put pressure on the aluminium market
Recent escalations in the Middle East are beginning to have a tangible impact on the global aluminium market. What is unfolding at a geopolitical leve...
Read more